

辊压成型生产线Linia CZS
Zeman
辊压成型生产线
Linia CZS
Zeman
出厂年份
2010
状况
二手
(完全功能)
位置
Częstochowa 




价格和位置
- 位置:
- Mariusza Bojemskiego 9, 42-202 Częstochowa, Polska
拨打
优惠详情
- 广告编号:
- A21299532
- 更新:
- 最近更新时间为 22.07.2026
描述
The line is from 2010. Modernization is being done in 2020.
Njdpfx Aoymampsc Dewl
ZEMAN CZS LINE SPECIFICATIONS
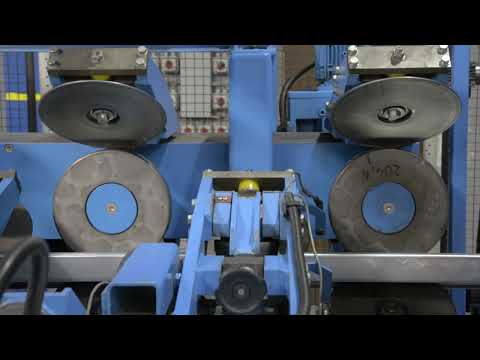
ZEMAN's flagship product, the fully automated "PURLIN" line, is used to produce open, cold-formed sections such as C, Z, and SIGMA, in various widths and shapes, thanks to fully automatic adjustment of the profiling rollers. Coils up to 750 mm wide and 1.25 mm to 3 mm thick sheet metal in grade S-390 and lower can be used as raw material. The machine is designed to produce components up to 15 m long. The width of the specially hardened profiling rollers is infinitely adjustable, using only dedicated software. A fully integrated "flying punching" device creates all types of mounting holes, and the entire process is continuous, meaning the material does not stop for individual operations such as punching holes or cross-cutting. To maintain production efficiency, the line speed is dynamically optimized. The machine decelerates and accelerates automatically without operator intervention.
A coil uncoiler with a maximum working load of 15 tons is mounted on a mobile trolley, enabling precise centering of the material strip before feeding it into the straightener.
The straightener, along with a crescent straightening system, allows for straightening the material, ensuring the required sheet flatness and reducing the crescent on the feed belt.
2. Punching Section
This section contains 5 double, "flying" punching portals, which can be equipped with 20 small (up to 40 mm) or 10 large (up to 100 mm) tools (punches and dies) for punching mounting holes.
A combination of these tools can also be used.
3. Pre-cutting Shear
A "flying" shear used to make preliminary holes for the cutting shear. This process is designed to maintain material continuity, resulting in a more precise profile shape, especially at its beginning and end. This is an adaptive guillotine that adjusts the width of the hole being cut to the width of the sheet metal strip.
4. Guide Carriage/SIGMA Modules
The guide carriage is used to center the sheet metal strip before entering the profiler. It is interchangeable
with the module for producing Sigma-shaped profiles. To produce S+ profiles,
the guide table should be removed and two Sigma modules inserted. These modules position
fully automatically and independently, left and right.
6. Rotary Cut-Off Guillotine.
The rotary cut-off guillotine with hook knives is used to finally cut the profile from the material strip
using the holes made by the pre-cutting guillotine. This is a "flying" guillotine,
so the sheet metal does not stop during the cutting process. Depending on the profile being produced, a properly oriented cutting cassette should be attached.
7. Receiving Table
The receiving table is used to automatically discharge the completed profiles from the roller conveyor. The elements are then manually arranged into a package. The design allows for easy bundling of the package. The table is designed to accept 15-meter profiles and allows for access by a forklift or overhead crane to collect the package of profiles.
供應商
注意: 免费注册或登录,以获取所有信息。
注册于: 2006
186 在线广告

发送询价
电话 & 传真
+48 34 30... 广告
这些广告您可能也感兴趣。
成功
您的消息已发送。
小广告


 Unterschleißheim
9,395 km
加工中心 - 立式
BRIDGEPORTVMC 610 XP
BRIDGEPORTVMC 610 XP
成功
您的消息已发送。
小广告


 Ulft
9,501 km
CNC板材加工设备
FicepTipo G25LG (S/N 36098)
FicepTipo G25LG (S/N 36098)

成功
您的消息已发送。
小广告


 Babberich
9,513 km
平面磨床 Ziersch - Z1030
ZierschZ1030
ZierschZ1030
成功
您的消息已发送。
小广告


 Beograd
8,960 km
分切生产线
GaspariniSlitter
GaspariniSlitter
成功
您的消息已发送。
小广告


 德国
9,303 km
5 轴数控加工中心
MazakVARIAXIS j-500
MazakVARIAXIS j-500
成功
您的消息已发送。
小广告


 德国
9,303 km
数控车床
GildemeisterCTX 200E
GildemeisterCTX 200E
成功
您的消息已发送。
小广告


 Idstein
9,490 km
CNC 车铣加工中心
DMGHSC 30 Linear mit EROWA Robot Compact 80
DMGHSC 30 Linear mit EROWA Robot Compact 80
成功
您的消息已发送。
小广告


 德国
9,303 km
数控车床
SpinnerTC 65-MC
SpinnerTC 65-MC
成功
您的消息已发送。
小广告


 Eschborn
9,477 km
立式加工中心
Deckel MahoDMF 250 linear
Deckel MahoDMF 250 linear
成功
您的消息已发送。
小广告


 德国
9,303 km
数控铣床
SpinnerVC 750
SpinnerVC 750
您的广告已成功删除
发生错误

Machineseeker-信任认证标志
什么是可信印章?
Machineseeker通过Machineseeker信任标志认证精选经销商。 在发放之前,Machineseeker 经验丰富的员工会进行标准化和全面的检测。
我们检查什么?

检查
营业执照或商业登记摘录
检查经销商的
邮寄地址
银行账户信息验证
主电话号码的
电话
可接通性验证
企业信用报告
不得显示任何负面特征
买家的投诉
可能导致认证标志被撤销这对您作为买家意味着什么?
通过 Machineseeker 信任标识,您作为买家无需自行检查,就可以识别出极有可能进行诚信且合法经营的可信经销商。
当然,在购买过程中仍可能出现分歧。 Machineseeker 对在 Machineseeker 上活跃的买家或卖家的法律违规行为不承担责任。